Industries
Explosion protection in the food and feed industry
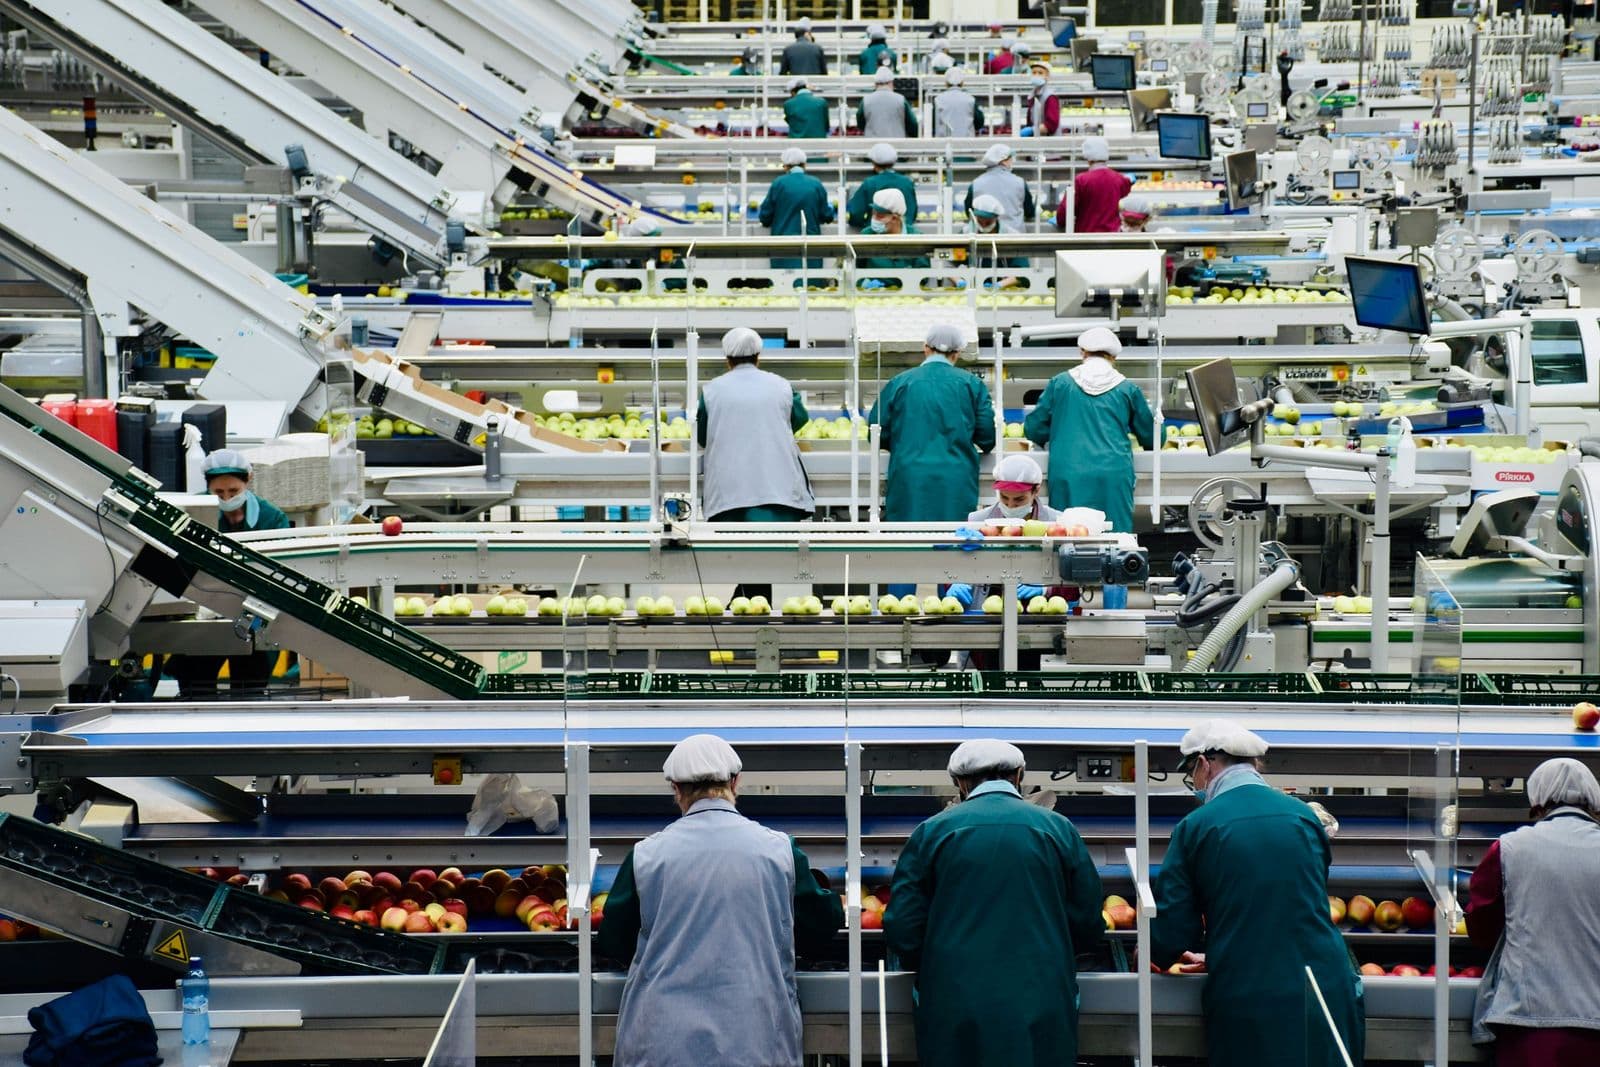
Food and feed production works with combustible dusts such as grain, flour, sugar, starch and feed dust. These dusts can form an explosive atmosphere inside silos, mills, bucket elevators and dust collectors.
A smaller primary explosion stirs up the dust settled on surfaces. That dust can spread through the hall and along interconnected equipment, causing a still larger and still more destructive secondary explosion. The documentation has to keep the dust zones, the Kst data, the protective measures and the cleaning regime current - that is what EPDS is for.
Industry experience
Sound familiar?
A bucket elevator or dust collector is replaced, but the zone classification and the protective measures do not follow the change.
The inside of the silos and filters is Zone 20, but nobody checks the sizing of the explosion venting.
Dust settles on surfaces around the hall, and it is not clear whether the cleaning regime is part of explosion protection.
You do not know whether the Kst value and minimum ignition energy of the dust being handled appear in the documentation.
Ahead of an audit you spend days gathering the zone drawings, the equipment list and the inspection certificates.
If any of these situations sounds familiar, another document is not what you need. What you need is a dependable system that tracks and documents the changes precisely.
Hazards
Typical explosion hazards in the food and feed industry
The industry deals almost exclusively with dust hazards, but the reactivity of those dusts varies widely:
| Hazard source | Where typical | Typical zone |
|---|---|---|
| Grain and flour dust | silos, mills, bucket elevators, conveyors | dust zone (20/21/22) |
| Sugar and starch dust | grinding, sieving, mixing | dust zone (20/21) |
| Feed dust | mixers, pelleting, conveying | dust zone (20/21/22) |
| Settled dust | hall surfaces, beams, the tops of equipment | dust zone (22), secondary explosion |
| Mechanical sparks and electrostatic charging | a foreign object in the mill, a bearing, pneumatic conveying | an ignition source in every zone |
How violent a dust is comes down to two characteristics of a dust explosion. The Kst value shows how quickly the pressure rises during an explosion. The minimum ignition energy shows how easily the dust ignites. These values are the basis on which protective measures are sized. The highest-risk equipment is the bucket elevators, the mills and the dust collectors, where the dust is often present at an explosive concentration. Interconnected equipment such as conveyors and ducts gives an explosion a path to propagate along.
When we help
Typical situations when it’s worth talking
The secondary explosion: the danger of settled dust
A primary explosion in a silo or filter stirs up the dust settled on the floor, the beams and the equipment. That cloud ignites, often causing a larger secondary explosion that runs the length of the hall. This chain reaction is what defines risk in the industry. Breaking it takes three things:
Remove settled dust. The cleaning regime is part of explosion protection: record it in the documentation rather than treating it as a separate task.
Isolate the equipment. Explosion isolation prevents an explosion from propagating along conveyors and ducts.
Relieve the explosion pressure. Explosion venting or suppression protects the equipment. The sizing is based on the Kst value of the dust.
The solution
How EPDS helps in the food and feed industry
EPDS brings explosion protection documentation into one system, from the dust data through to the protective measures:
Dust, zone and equipment register in one place.
EPDS holds the Kst and MIE data of the dusts, the zones and every Ex device in one place, and makes them searchable.
Management of change.
The software traces the effect of new equipment or a new process through the zones and the protective measures.
A register of protective measures and the cleaning regime.
EPDS also records the status of venting, suppression, isolation and the cleaning regime.
No more overdue inspections.
The system gives notice of inspections as they fall due, and records the ones completed.
An audit-ready report in one click.
EPDS assembles the report of zones, equipment and inspections, per site too.
Documentation that is always current.
You can look back at any time to see who changed what, and when.
Knowledge hub
Before you decide, get informed.
Our expert knowledge base explains the concepts of explosion protection clearly.
FAQ
Frequently asked questions
What is the Kst value, and why does it matter?
Kst characterises how violent a dust explosion is: it shows how quickly the pressure rises during one. It is the basis for sizing explosion venting and suppression, which is why the Kst value of the dusts being handled has to appear in the documentation.
Why is settled dust dangerous?
A primary explosion stirs up the dust settled on surfaces, and the resulting cloud can cause a larger secondary explosion. That is why the cleaning regime is an integral part of explosion protection, not a separate task.
Which equipment carries the greatest risk?
Bucket elevators, mills and dust collectors, because the dust in them is often present at an explosive concentration. It is worth protecting this equipment with isolation as well, so that an explosion cannot propagate further.
When does the zone classification have to be redone?
At every change that affects the explosion hazard: new equipment, a change of process, a different raw material, or a modification to the conveying or the extraction. In EPDS this is part of management of change.
Does a mill or feed plant need explosion protection documentation?
Yes. Wherever combustible dust can create an explosive atmosphere, the documentation is mandatory under decree 3/2003. (III. 11.), and it has to be kept current.
Let’s talk it through — free consultation
In a short, free conversation we show you the EPDS system mapped onto your processes, and review where your documentation stands today.